If you’re in the industrial game, you know ball linear guides are the unsung heroes of so many machines—CNC routers, automated assembly lines, 3D printers, even medical lab equipment that moves tiny vials with pinpoint precision. But here’s the thing: I’ve seen way too many clients write off their maintenance bills as “just part of the cost of running gear like this.” As someone who’s been selling ball linear guides for the last 8 years, I’m here to tell you that 70% of those maintenance headaches are totally avoidable. We’re not talking about skipping oil changes or cutting corners—we’re talking about smart, small tweaks that keep your guides running smooth, cut costs, and keep downtime to a minimum. Ball Linear Guide

First off, let’s get one thing straight: most maintenance costs for linear guides don’t come from parts breaking. They come from stuff you’re probably doing wrong without even realizing it. Like, did you know over-greasing is a bigger issue than under-greasing? I can’t tell you how many times a client will dump a glob of grease on their guide “just to be safe” and end up with gunk buildup that traps dust and debris, which wears out the ball bearings faster. Or the opposite—they wait so long to re-lube that the metal-on-metal friction causes the raceways to score, and suddenly they’re replacing the whole assembly instead of just a grease nipple. So let’s start with the basics that everyone skips: choosing the right lube, and using the right amount at the right time.
First, pick lube that’s actually made for ball linear guides, not just generic grease from the auto shop. I’ve seen clients grab a cheap multi-purpose grease because it’s on sale, and that’s a recipe for disaster. General greases are too thick or too thin for the tight tolerances of linear guides—too thin, and it runs off under heavy load; too thick, and it creates that gunk I mentioned earlier. The right lube is usually a synthetic grease with anti-wear additives specifically formulated for linear motion systems. And forget “once a month forever”—track your machine’s usage. If your CNC router runs 24/7, you’ll need to re-lube every 100-200km of travel, not every 30 days like a generic schedule. If your 3D printer only runs 8 hours a day, you can stretch it to every 800km. Pro tip: if you notice unusual noise (not the normal hum of a machine, but a high-pitched squeak or grind) or a drop in positioning accuracy, that’s your guide begging for lube—don’t wait for the scheduled time. And about that amount: a golf-ball size glob is too much. For standard guides, it’s just enough to fill the internal lubrication channels, usually 1-2 pumps from a grease gun, or a thin film wiped along the rail if you’re manually applying. Over-greasing also leads to more heat buildup, which expands the metal and messes with the guide’s tight fit—more wear, more cost, you get it.
Next up: keeping debris out. This is the #1 cause of early linear guide failure, hands down. Dust, metal shavings, wood chips, even plastic fumes from 3D printers—these tiny particles act like sandpaper between the balls and the raceways, wearing down the grooves until the guide can’t hold position anymore. And guess what? Cleaning out that damage later is way more expensive than preventing it. The easiest, cheapest fix here is proper sealing. A lot of machines come with basic rubber scrapers on the guide blocks, but those only do half the job. If you’re running a high-dust environment—like a wood shop, a metal fabrication floor, or a facility with lots of paper or plastic dust—upgrade to double-lip seals or even metallic wipers. I once had a client in the aerospace industry who was replacing 4 guides a year because of metal shavings, and after switching to our heavy-duty metallic wipers, they haven’t had to replace a single one in 3 years. The cost of the seals? Less than 5% of the cost of a new guide. Another quick win: install a simple cover over the rail when the machine isn’t in use. Even a cheap plastic or aluminum cover keeps debris off when the machine’s idle, and it takes 2 minutes to pull off when you’re ready to run. I know, it sounds obvious, but you’d be shocked how many factories leave their machines exposed 24/7 because “it’s easier” or they forgot.
Wait, let’s talk about installation, because so many maintenance costs start the day the guide is put in. A lot of DIYers or even small maintenance teams will just bolt the rail down and call it a day, but if the rail isn’t aligned properly, you’re already setting yourself up for failure. If the rail is even slightly crooked (like a 0.1mm gap over a 1m length), the balls are going to wear unevenly, and you’ll have to replace the whole guide way sooner than you should. Proper installation means using a precision level to check alignment, torquing the mounting bolts to the manufacturer’s specs (not just as tight as you can with a wrench—over-torquing bends the rail, under-torquing makes it shift), and making sure the surface the rail is mounted on is flat and free of burrs or debris before you even put it down. I’ve had clients come to me saying their guides are “cheap garbage” because they’re failing in 6 months, only to pull the old guide off and see that the mounting surface had a 0.5mm dent that twisted the rail. That’s not the guide’s fault—that’s installation error. And fixing that dent later is way cheaper than replacing a whole guide set. Also, don’t mix guide blocks from different batches if you need to replace one down the line. Even small variations in manufacturing mean blocks from different batches won’t align perfectly, so mixing them causes extra friction and wear.
Another big one: monitoring load and speed, because overworking a linear guide is like running a car at max speed every single day—it’s going to break faster. A lot of people size their guides based on the maximum load the machine can handle, but they forget that the load is dynamic. If your machine is lifting a 50kg load that’s centered on the guide, that’s fine, but if the load is off-center, that creates uneven pressure on the balls, leading to accelerated wear. So calculate the actual dynamic load your guide will see, not just the max static load. Dynamic load is what the guide experiences when it’s moving, so it’s usually lower than static, but if you don’t account for off-center loads, acceleration forces, and even shock loads (like if your machine slams to a stop suddenly), you’ll end up with guides that wear out too fast. Also, speed matters. Linear guides have a maximum recommended speed, and running them faster than that creates more heat and more centrifugal force on the balls, which wears out the raceways. If you need higher speed, talk to us about a high-speed ball guide design—we build them with optimized ball retainers that reduce friction at speed, so you don’t have to replace guides every year just to keep up with production.
Wait, what about replacement parts vs. whole assembly? This is a big cost saver that a lot of people miss. When a guide block goes bad, a lot of people just replace the whole rail and block set, which is way more expensive than it needs to be. Most ball linear guide blocks are designed so you can just replace the ball circuit or the internal components, not the whole block, as long as the rail isn’t damaged. I had a client last year who thought he needed $2,000 worth of new guides for his packaging line, but we came out and checked—all the damage was just the ball bearings in the blocks, so we replaced just the blocks’ internal circuits for $300, and he was good to go. That’s a 85% cost saving right there. The key here is regular inspections—every 3 months, pull the guide blocks off, check for any scoring on the rail (not just the blocks), and if the rail is fine, don’t replace it. We also recommend keeping a small stock of common replacement parts (ball circuits, seals, lube) on hand so you don’t have to rush order whole assemblies when something goes wrong, which usually costs more because of expediting fees.
Let’s also talk about environment, because some maintenance costs are directly tied to where your machine lives. If your machine is in a high-temperature environment—like a metal foundry or a paint shop—the grease breaks down faster, and the metal expands, which changes the guide’s clearance. For high temps, use a high-temperature synthetic lube rated for your environment, and re-lube more frequently. If it’s a cold environment (like a freezer or a northern warehouse in winter), regular grease gets too thick, so you need a low-temperature lube that flows properly when it’s cold. Even the humidity matters—high humidity can cause rust on the steel rails, which is another big wear factor. If you’re in a humid area, add a rust inhibitor to your lube, or use stainless steel rails if moisture is a constant issue. I’ve had a lot of food processing clients switch to stainless steel guides because their old steel ones were rusting from washdowns, and their maintenance costs dropped by 40% in the first year. That’s a no-brainer.
Wait, let’s bust a common myth here: “cheaper guides mean lower maintenance costs.” That’s not true at all. A cheap guide might have lower upfront cost, but if it wears out in 6 months, that’s way more maintenance and replacement cost than a slightly more expensive guide that lasts 5 years. I see this all the time— a client will buy a set of guides from a no-name supplier for $100 each, instead of our $150 ones, and 6 months later they’re back buying new ones, plus paying for downtime while their line is down. The real cost of a guide isn’t the upfront price—it’s the total cost over its lifespan, including maintenance, replacement, and downtime. So when you’re picking guides, don’t just look at the sticker price. Look at the load rating, the sealing, the material, and the expected lifespan, because that’s what will keep your maintenance costs low long-term.
Another quick tip: train your maintenance team. A lot of the mistakes I see are because people don’t know what to look for. I’ve had new maintenance guys over-torque bolts, or use the wrong grease, or forget to check seals because they were never shown. We do free quick training sessions for all our clients on proper lube, inspection, and installation, because it saves both of us money in the long run. If your team knows the basics, they’ll catch small issues before they become big, expensive problems. Like, if a seal is wearing out, they can replace it for $10 before it lets in dust that ruins the whole guide for $500. It’s the same as changing the oil in your car—small, regular checks prevent huge repair bills.
Let’s wrap this up with a quick checklist you can use right now, no fancy tools needed. First, check your lube: are you using linear-guide specific synthetic grease? Are you applying the right amount, not too much, not too little? Second, check your seals and covers: are your scrapers intact? Do you have double lips if you’re in a dusty/humid environment? Is the rail covered when not in use? Third, check installation: is your rail aligned? Are mounting bolts torqued to spec? Is the surface under the rail flat? Fourth, check load and speed: are you exceeding the guide’s dynamic load or maximum speed? Do you have off-center or shock loads that you’re accounting for? Fifth, replace parts not whole assemblies when possible: if the rail is good, just swap the ball circuits in the blocks instead of the whole thing.
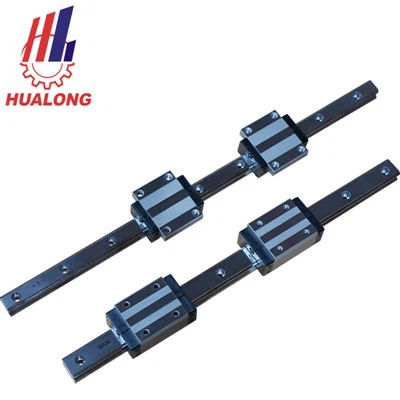
At the end of the day, reducing ball linear guide maintenance costs isn’t about skipping things—it’s about being smart, intentional, and proactive. It’s about spending a little time and a little money upfront on the right lube, seals, and installation, so you don’t have to spend thousands in repairs and downtime later. I’ve been in this game long enough to know that most clients want their machines to run smooth, not have to fix them every other week. That’s exactly what we build our guides to do, and we’re here to help you make the most of yours. If you’re tired of overpaying for maintenance, dealing with unexpected downtime, or just want to optimize your linear guide setup, hit us up to chat through your specific needs. We can help you figure out exactly what tweaks will work for your machine, your environment, and your budget.
Roller Square Linear Guide References:
- Linear Motion Systems: Selection, Application, and Maintenance. Industrial Press, 2021.
- Ball Screw and Linear Guide Performance in Industrial Environments. International Journal of Machine Tools and Manufacture, vol. 58, no. 3, 2018, pp. 212-225.
- Maintenance Best Practices for Linear Motion Components. Motion Control Association, 2020.
- The Impact of Contamination on Linear Guide Wear and Service Life. Wear, vol. 392-393, 2017, pp. 117-125.
- Sizing Linear Guides for Dynamic Loads and Speed: A Practical Guide. Society of Manufacturing Engineers, 2019.
Fujian Province Hualong Machinery Co., Ltd.
As one of the leading ball linear guide manufacturers and suppliers in China, our products have good reputation in the market. Please rest assured to wholesale bulk ball linear guide made in China here from our factory. Welcome to view our website for more information.
Address: Huangshi Industrial Park, Putian city, Fujian Province, China
E-mail: jenkin@hualongm.com
WebSite: https://www.guidelinear.com/
