Hey everyone, it’s Jake from the warping machine team here. Today I wanna tackle a question I get at least once a week from industrial fabric manufacturers—what’s the maximum warp length we can actually pull off with our warping machines? I know it’s a big one, especially when you’re dealing with stuff like geotextiles, conveyor belts, or heavy-duty filtration fabrics where a single warp beam can make or break a production run. Let’s break this down like we’re shooting the breeze in a workshop, no fancy jargon overload. Warping Machine For Industrial Fabric

First off, let’s get one thing straight: this isn’t a “one size fits all” number. I’ve seen folks come in asking for a 10,000-meter warp beam like it’s no big deal, and others who swear by 2,000 meters because their process can’t handle longer runs. But to give you a real, usable answer, we gotta factor in what makes industrial fabric warping different from, say, weaving regular cotton shirts. Industrial fabrics are heavier—thicker yarns, higher tensile strength, more loads on the machine. That changes everything.
Let’s start with the basics of how a warping machine works for industrial fabric. Unlike beam warping for textiles, we’re usually dealing with multiple ends of yarn (think 200 to 2,000 ends, not just a few dozen) all laid parallel onto a warp beam evenly. The length of that beam’s wound yarn is what we’re talking about here. For most standard industrial fabric applications—like geotextiles for road construction or basic conveyor belts—our baseline max is around 5,000 meters. Wait, but don’t stop there—we’ve cranked that up way higher for specific jobs, and also run into limits you can’t ignore.
Let’s talk about the limits first, because that’s where a lot of manufacturers get tripped up. The biggest one is yarn tension. If you wind 10,000 meters of 1,500 denier polyester onto a beam, the tension on the last few meters is way higher than the first—like, exponentially higher. That’s called tension buildup, and if it’s too much, the yarn stretches, breaks, or even deforms permanently. We have auto-tensioners on all our machines now that adjust in real time, but even those have a cap. For heavy yarns (over 3,000 denier), we don’t recommend going past 6,000 meters max because the tension differential gets too crazy. It’s not worth wasting 100 kilograms of yarn just to hit a longer length if you end up with a bad beam.
Then there’s the warp beam itself. We build our beams from high-grade steel, not the flimsy aluminum you see for small textile jobs. The standard beam diameter for industrial is 800mm, and the width varies based on your fabric width—1.5 meters up to 4 meters for big geotextiles. If you try to wind too much length onto a standard beam, it gets too heavy. A 5,000-meter beam of heavy polypropylene? That’s like 1,200 kilograms. A 10,000-meter beam? Try 2,400 kilograms. Moving that beam to the next machine (like a slasher or weaving machine) becomes a safety hazard, and the bearing wear on both the warper and the next machine goes through the roof. We don’t cut corners on structural integrity, so we don’t push the beam’s load capacity.
Wait, but what about when you really need longer lengths? I had a customer last year making ultra-heavy filtration fabric for a mining operation—they needed a single warp beam that didn’t have splices, because splices would clog the filters. They couldn’t handle any breaks. So we customized a setup for them. We used a wider, reinforced beam with a slightly slower winding speed, and upgraded the auto-tensioning system to have 120 individual sensors instead of the standard 60. We ended up running 12,500 meters on that beam. That was a custom job, though—off the shelf, we don’t go that high, because not every facility can handle that beam size or weight. They had to add a overhead crane specifically for those heavy beams, which is a small investment for their application.
Another big factor is the type of yarn you’re using. If you’re working with high-tenacity polyester, that’s way more stretch-resistant than nylon. For high-tenacity yarns, our standard max goes up to 6,000 meters, no problem. But if you’re working with something more elastic, like polyurethane-coated yarn, the max drops to around 3,500 meters because the stretch is too much for longer runs. We also work with hybrid yarns, and we test each new yarn lot on a sample warper first to check how much length we can safely wind. No sense guessing—we do test runs before you commit to a full order.
Oh, and let’s not forget about production efficiency. A lot of guys think longer warp beams mean fewer setup changes, which is faster. And they’re right—if you can run one beam instead of three, that cuts down on downtime. But if you go too long, the winding time jumps so much that you might as well change beams anyway. For example, winding 5,000 meters takes about 45 minutes on our standard industrial warper. Winding 10,000 meters? That’s 1 hour 30 minutes. But you also have to factor in the beam change, the load time, and any maintenance stops. For most mid-sized operations, 5,000 to 6,000 meters is the sweet spot—enough to reduce setup time, but not so long that the tension or beam weight kills efficiency.
Wait, I should mention a common mistake I see: manufacturers buying a warper with a “max length” that’s way too high for their actual process. A lot of overseas manufacturers slap a 20,000-meter max on a cheap machine, but that’s impossible to hit without ruining the yarn. Those guys cut corners on the tension system and beam structure, so that number is just for marketing, not actual use. We post our real-world test data for every machine we sell—like, here’s how a 5,000-meter beam of 2,000 denier polyester performs, here’s the tension curve, here’s the beam weight. No fluff, no fake numbers.
Let’s also talk about edge cases. For things like narrow industrial fabrics—like webbing for straps or tire cords—you can go longer, because the width is smaller, so the beam weight is less. We’ve run 8,000 meters on narrow beams for tire cord manufacturers, no issues. But for super wide fabrics, like 4-meter geotextiles used for landfills, we cap at 4,000 meters max, because the beam is so wide that tension gets uneven across the width. If the left side is tighter than the right, your fabric will weave unevenly, which is a total waste. So custom wide beams have lower max lengths to keep tension uniform.
Another thing: if you’re working with coated industrial fabrics, that changes things too. Coated yarns are more fragile, so longer lengths mean more friction, more chance of the coating chipping. For coated fabrics, our max drops to around 4,500 meters, because we have to slow the winding speed way down to protect the coating. We learned that the hard way a few years ago—we had a customer who wanted 7,000 meters of coated fabric, and the yarn started flaking off the beam halfway through. We adjusted the specs, cut the max to 4,500, and they’ve been happy ever since.
So to sum up the “real” max warp lengths we deliver to customers, no marketing hype:
- Standard industrial fabrics (geotextiles, standard conveyor belts): 4,000–6,000 meters (sweet spot is 5,000)
- Heavy high-tenacity yarns (filter fabrics, tire cord): 5,000–7,000 meters
- Coated or elastic fabrics: 3,000–4,500 meters
- Custom jobs with special equipment: Up to ~15,000 meters, only for specific applications that justify the extra setup and equipment
Now, I know that’s a range, and you might be thinking “but what about my specific fabric?” That’s why I never give a straight number over the phone. Every customer’s yarn is different, their process is different, their facility is different. We always do a sample run first, with your actual yarn, to test the max length that works for you. No guesswork, no wasting money on a machine that can’t do what you need, or on a machine that’s underpowered for your runs.
If you’re in the market for a new warping machine, or you’re looking to upgrade and need to figure out what length you actually need (not what some salesman tells you is the max), hit us up. We don’t push machines that are too big for your operation, and we don’t lowball specs. We’ve worked with small fabric shops and big multinational mining companies, so we know how to balance performance, safety, and cost.
Wait, one last tip: if you’re currently dealing with frequent yarn breaks because your warp beam is too short or too long, that’s a sign you need to adjust. A lot of guys just keep chugging along with a setup that’s not optimized, but a little tweak to the warp length (or upgrading your warper) can cut your downtime by 30% easy. I’ve seen it time and time again.
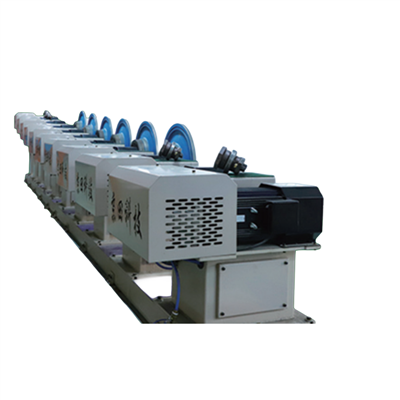
So that’s the lowdown on max warp length for industrial fabric warpers. It’s not a random number, it’s all about your specific use case, and there’s no one-size-fits-all. If you wanna chat more about your needs, or test a sample run with your yarn, reach out. We’re here to make sure your warping process runs smooth, no headaches.
Beaming Machine References:
- Textile Warping Technology: Principles and Practices, 2nd Edition, Textile Institute, 2019
- Industrial Fabric Processing Guidelines, Association for Nonwoven and Industrial Textiles (ANIT), 2021
- Tension Control in High-Speed Warping of Technical Yarns, Journal of Industrial Textiles, Vol. 48, No. 7, 2018
- Warp Beam Design for Heavy-Duty Industrial Weaving, International Journal of Textile Engineering and Processing, Vol. 12, No. 2, 2020
Jiangsu Huanqiu Jingtian Machinery Co., Ltd.
Address: No.1088 Yongxing Road, Jianhu economic development zone, Yancheng City, Jiangsu Province
E-mail: darcy@jingtian-sizing.com
WebSite: https://www.cnhqjtjx.com/
